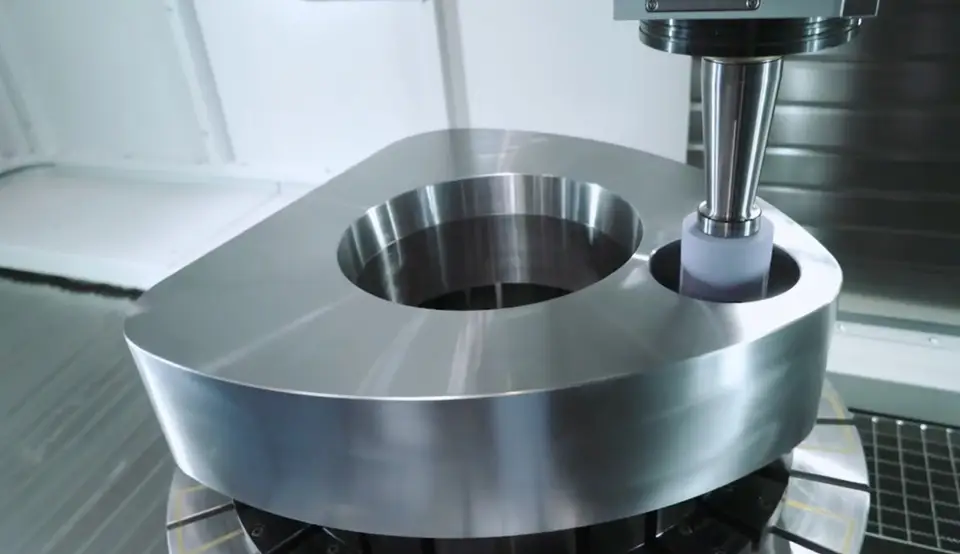
 Made on OpenSpindle
Precision Grinding partMade on OpenSpindle
Abrasive grinding holds some of the tightest tolerances and finest surface finishes in machining, including on hardened materials that are slow and difficult to mill or turn after heat treat. Upload your part or print and we'll send you one matched quote from a qualified manufacturing partner.
STEP · STL · IGES · DWG · DXF · SLDPRT · and more
No CAD file? Describe your project instead
Made on OpenSpindlePrecision grinding is a machining process that uses a spinning abrasive wheel to remove a thin, controlled layer of material. It holds tighter tolerances and finer finishes than milling or turning, to about ±0.0001 in and 4 to 8 µin Ra, and works on hardened steel, carbide, and ceramics, which makes it the standard finishing step after heat treat.
Last reviewed
Send a part and get a real price. Nothing to commit to, no cost to ask.
One lead from quote to delivery who has sourced it before.
NDA on request. Files shared only with matched shops.
A CAD file or a sketch. Free quote in about 24 hours.
The best-fit shop from our network makes it, on your timeline.
Inspected, shipped and tracked in your inbox.
Grinding uses a spinning abrasive wheel to remove a small, controlled amount of stock, which is why it holds tolerances and finishes that milling and turning struggle to match.
| Design rule | Typical spec | Why |
|---|---|---|
| Achievable tolerance | to ~±0.0001 in (0.0025 mm) | Light abrasive cuts and stiff machine setups hold tenths where milling and turning usually struggle. |
| Surface finish | to ~4-8 µin Ra | Fine wheel grits and slow finishing passes produce a mirror-like surface. |
| Flatness / parallelism | to ~0.0002 in | Surface grinding is the standard way to true two faces flat and parallel. |
| Hardened material capability | grinds hardened steel, carbide, ceramics | Abrasive cutting removes material regardless of hardness, unlike a single-point tool. |
| Grind stock allowance | leave ~0.005-0.015 in for grinding | Rough the part close on a mill or lathe first, then leave finish stock for the grinder to clean up. |
Typical starting points; a shop confirms against your part, material, and hardness.
The shop picks the method from your CAD, and the quote tells you which.
Grinding shops on OpenSpindle finish hardened tooling, shafts, gauges, and precision components for demanding industries, including AS9100 and ISO 13485 shops.
| Instead of | Send this |
|---|---|
| "Ground part, need a quote" | "4140 steel, hardened 50 HRC, surface grind top face flat and parallel to 0.0002 in, qty 10" |
| "Needs to be round and precise" | "O1 tool steel shaft, cylindrical grind ⌀0.500 in ±0.0002, 8 µin Ra finish" |
| "Lots of small pins, tight tolerance" | "303 stainless dowel pins, centerless grind ⌀0.125 in ±0.0002, qty 2,000" |
Say the material and hardness, the surface being ground, and the tolerance and finish that matter. Grinding is often called out for one critical feature, not the whole part.
When another process fits better than grinding.
| Process | Best for | Typical volume | Choose it over Precision Grinding when |
|---|---|---|---|
| CNC Machining | General tolerances, soft or as-machined finish | Prototype to production | A milled or turned finish and tolerance suffice, typically before heat treat. |
| EDM & Wire EDM | Complex hard-metal detail, internal features | Prototype to production | The part needs sharp internal detail in hardened material with no cutting force. |
| Lapping and honing | The final finish on flats and bores | Low to production | The part needs the ultimate flatness or bore finish beyond what grinding alone leaves. |
The design choices that move your price and lead time.
A surface grinder holds a part on a magnetic chuck and passes a wheel over the top face, the go-to way to make two faces flat and parallel after heat treat or welding distortion.
A part turns between centers or in a chuck while the wheel grinds an outside diameter, shoulder, or taper to final size, common for shafts, pins, and rollers.
Parts feed between two wheels with no chuck or centers needed, which removes setup time per part and makes it economical for grinding large batches of pins and shafts to a consistent diameter.
Grinding is slower and pricier per surface than milling or turning. Spec grinding for the one or two features that carry the tight tolerance or finish, and leave the rest at a standard machined tolerance.
Precision grinding cost depends on the tolerance and finish required, the amount of stock to remove, the part's size and shape, and the material's hardness. Grinding removes material in light passes, so a part that arrives with heavy stock or a lot of heat-treat distortion takes longer than one machined close to size. Tighter tolerances and lower Ra finishes need slower passes, more wheel dressing, and more measurement between passes. Surface grinding of flat parts, cylindrical grinding of shafts, and centerless grinding of pins each run at different rates, and centerless work can become inexpensive per part at volume. Hardened tool steel and carbide grind slower and wear wheels faster than soft steel, and carbide usually calls for diamond wheels. Fixturing for thin or odd-shaped parts adds setup. Upload your print with the ground features called out and OpenSpindle returns one quote from a matched grinding shop.
Precision grinding lead time depends on where grinding sits in the part's route, the matched shop's queue, and how much inspection the tolerances require. Grinding is usually a finishing step, so a hardened part may be machined, sent out for heat treatment, and then ground, and each stage adds time. If you send parts that are already hardened, the grind itself is often a short operation compared with the steps before it. Tight tolerances on flatness, parallelism, or roundness need careful measurement, and certified inspection reports add time at the end. Large parts or high quantities of centerless-ground pins take more machine time. After you upload your print, OpenSpindle usually returns one quote in about 24 hours, and the quote shows a lead time for the work you need. Note any required date, and say whether you are supplying the parts or need them made from stock, so the full route is planned.
Shops that do this work · partner with OpenSpindle
We route this work to specialists. If any one of these describes your shop, we have matching RFQs we would send you.
Upload your part or print and we'll send you one matched quote from a qualified manufacturing partner set up for surface, cylindrical, and centerless grinding.
STEP · STL · IGES · DWG · DXF · SLDPRT · and more
No CAD file? Describe your project instead
Precision grinding uses a spinning abrasive wheel to remove a thin, controlled layer of material, holding tolerances and surface finishes tighter than milling or turning. It is the standard way to finish a part after heat treat, when hardening has thrown off dimensions and an abrasive process is the usual way to bring them back.
Surface grinding flattens and finishes a face, typically on a magnetic chuck, and is used to true up flat and parallel surfaces. Cylindrical grinding rotates a part between centers or in a chuck to grind an outside diameter, shoulder, or taper round and to size. Centerless grinding feeds round parts between two wheels with no chuck or centers, which makes it fast and economical for grinding large quantities of shafts or pins to a consistent diameter.
Surface and cylindrical grinding commonly hold tolerances to about ±0.0001 in and surface finishes down to roughly 4-8 µin Ra, well beyond what a mill or lathe alone can hold.
Yes. Grinding is the standard finishing process for hardened tool steel, carbide, and ceramics, since abrasive cutting removes material largely regardless of hardness, where a single-point cutting tool needs special inserts and wears quickly. Most hardened parts are ground after heat treat to bring dimensions back into tolerance.
A common allowance is 0.005-0.015 in per surface, roughed close on a mill or lathe before heat treat, then removed by the grinder afterward to true up size and finish.
STEP, IGES, X_T, DWG, DXF, or a dimensioned PDF. Include material and hardness, the surface or feature being ground, its tolerance and finish, and quantity.
Comparing manufacturing services? See Xometry alternatives