 Made on OpenSpindle
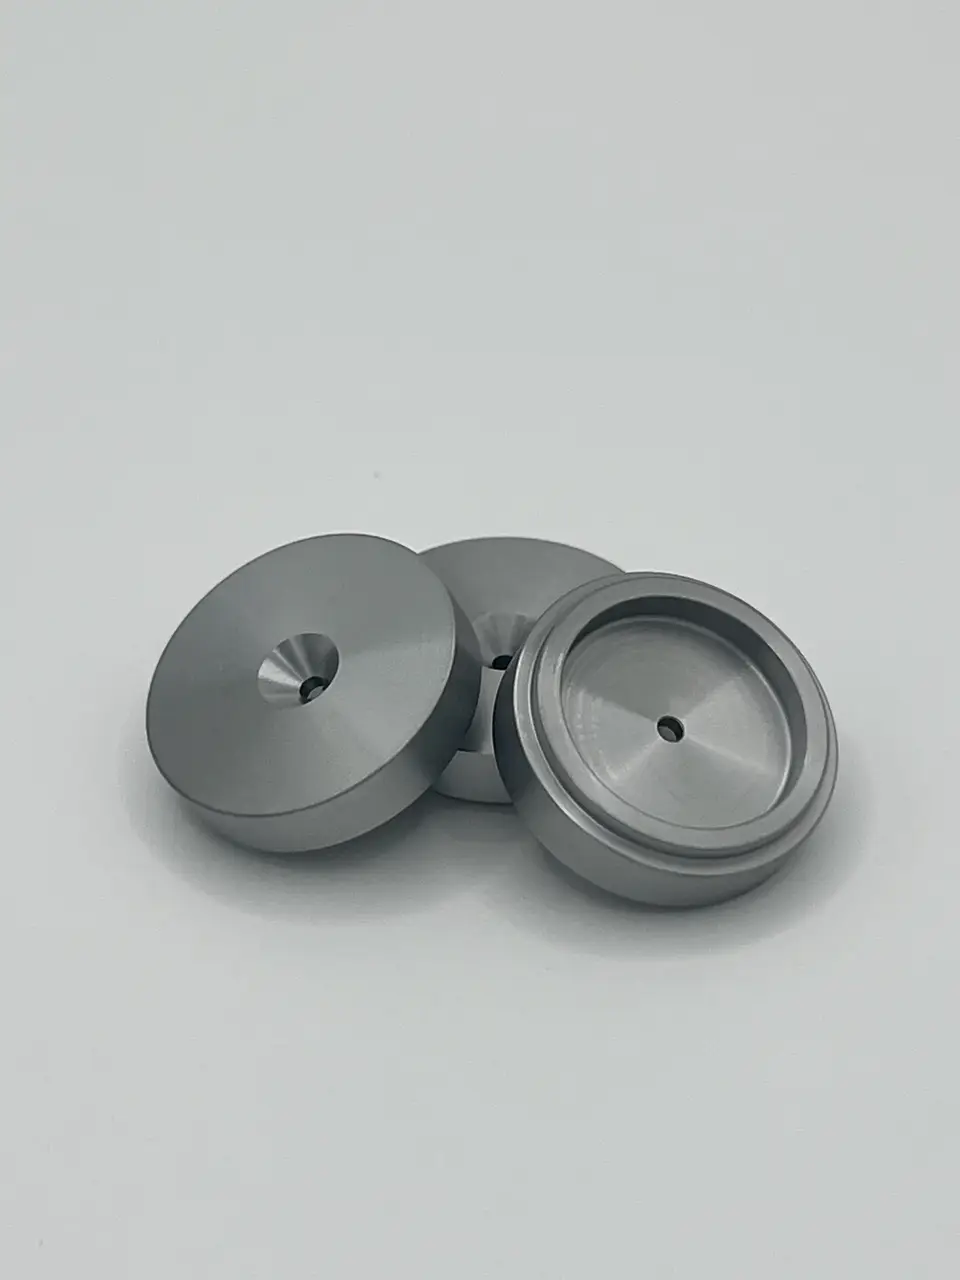
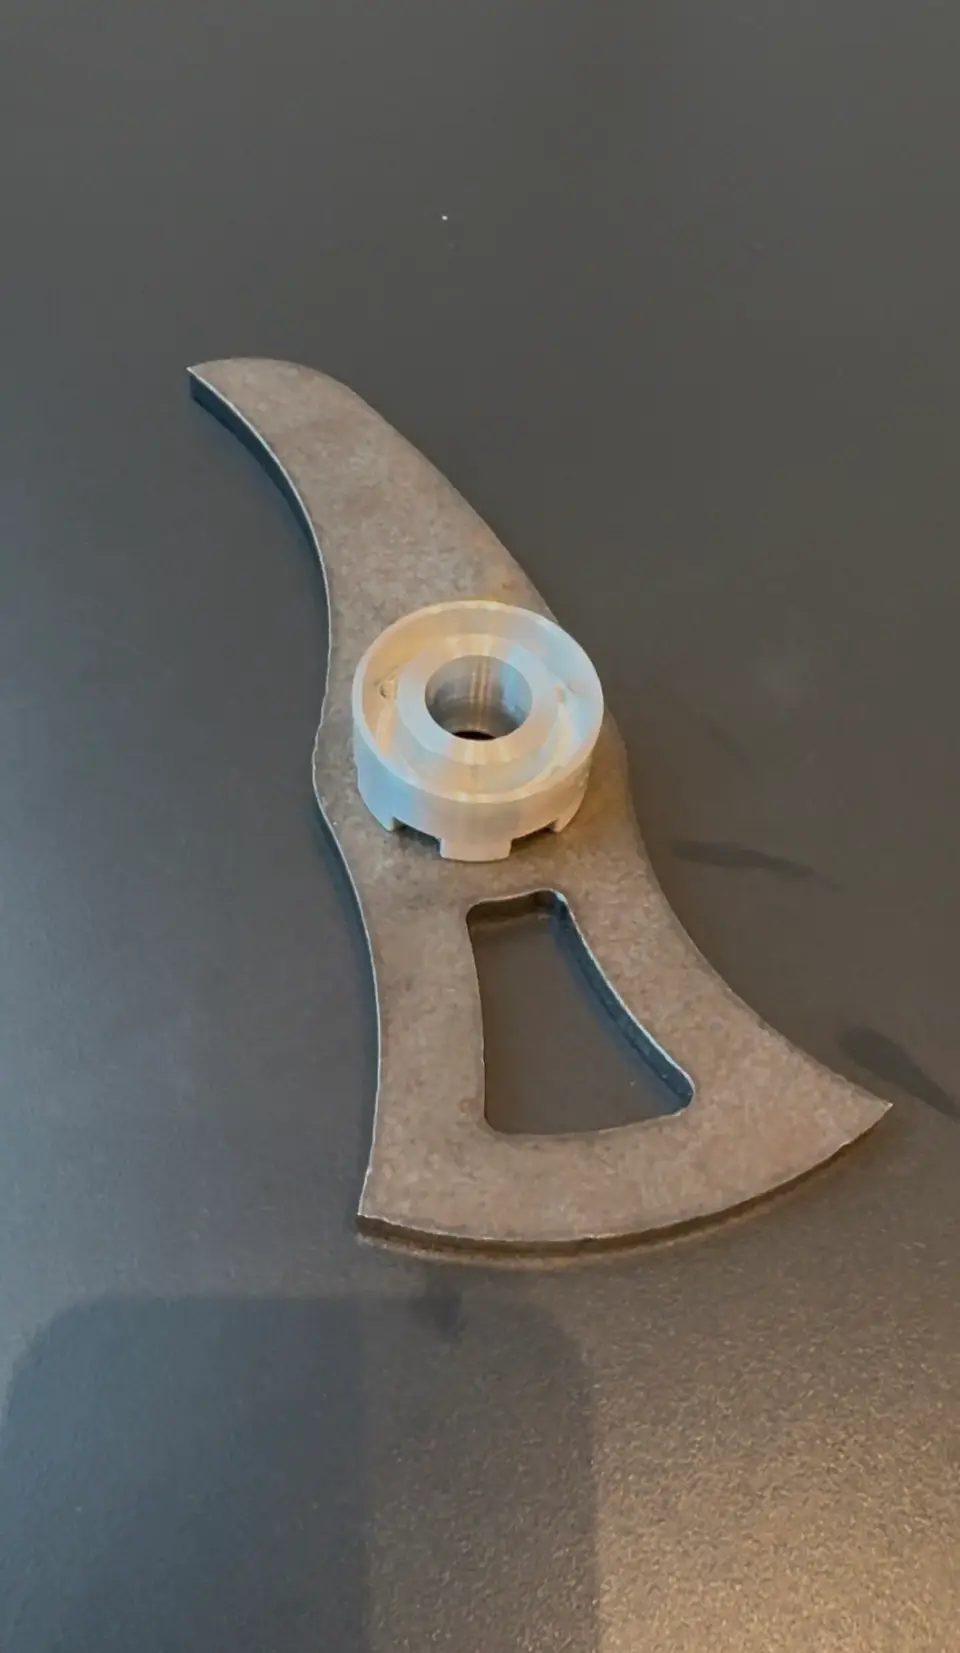
Small Machined CapsMolybdenum · EDM & Wire EDM
Tens to a few thousand parts without a big tooling bill. Low-volume production is the bridge between a prototype and full production, and the right process depends on your material, geometry, and volume. Upload your CAD files or drawings and we'll send you one matched quote from a qualified manufacturing partner.
STEP · STL · IGES · DWG · DXF · SLDPRT · and more
No CAD file? Describe your project instead
Made on OpenSpindleSend a part and get a real price. Nothing to commit to, no cost to ask.
One lead from quote to delivery who has sourced it before.
NDA on request. Files shared only with matched shops.
There is no single "low volume" process. Each of these fits a different combination of material, finish, and run size, and it is common to mix methods across one bill of materials.
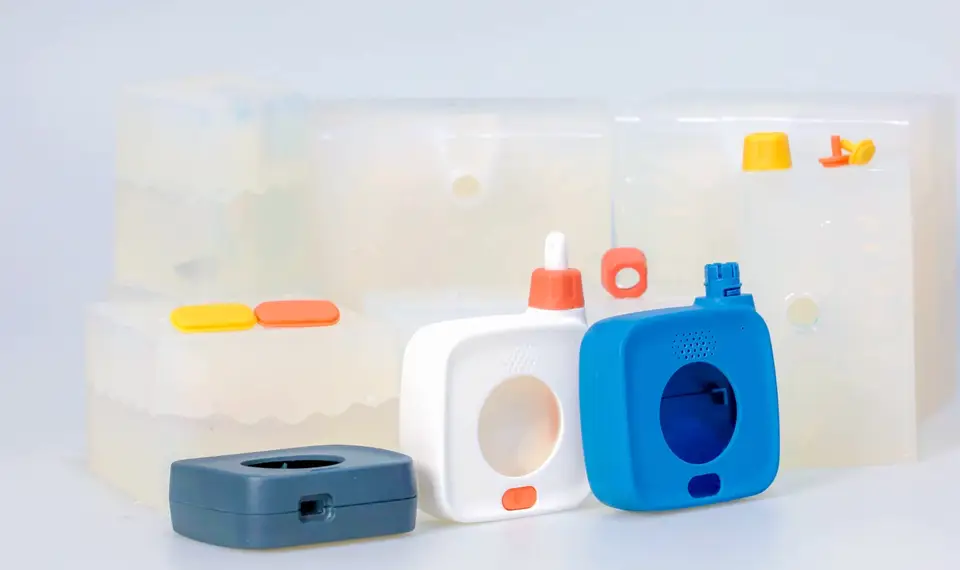 Urethane CastingTypical Lead time1-3 weeksVolume10-200Molded feel from a cheap silicone tool cast off a master pattern, no steel or aluminum mold needed.Prototype/Bridge MoldingTypical Lead time3-5 weeksVolume100-10,000An aluminum tool bridges the gap to production while a hardened steel mold is being cut.
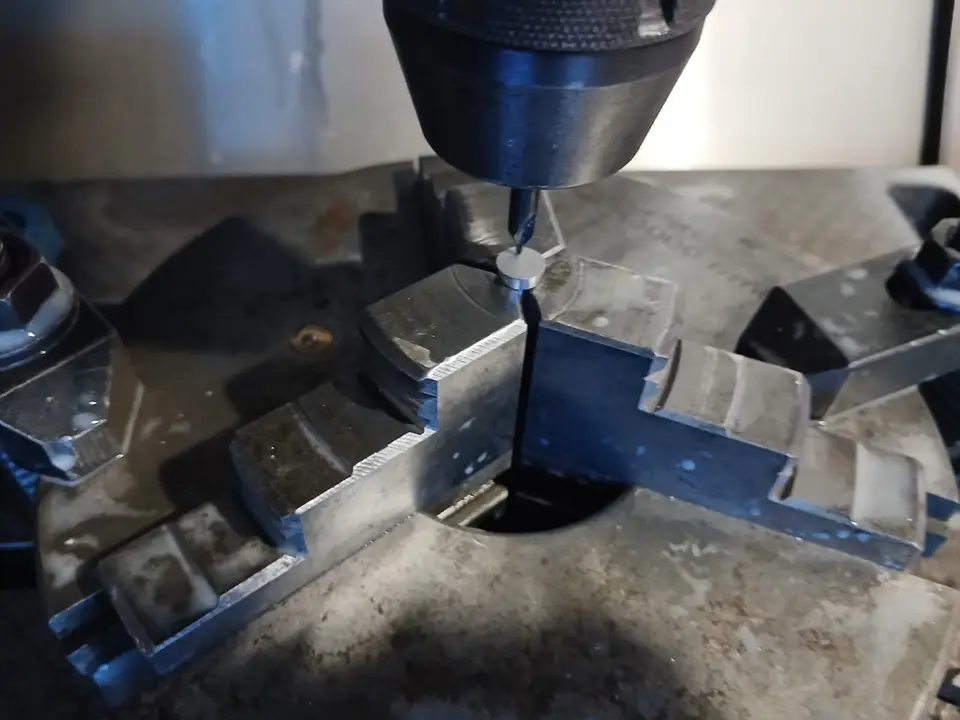 CNC MachiningTypical Lead time1-2 weeksVolume1-1,000No tooling at all, holds tight tolerances, and runs in nearly any metal or plastic.
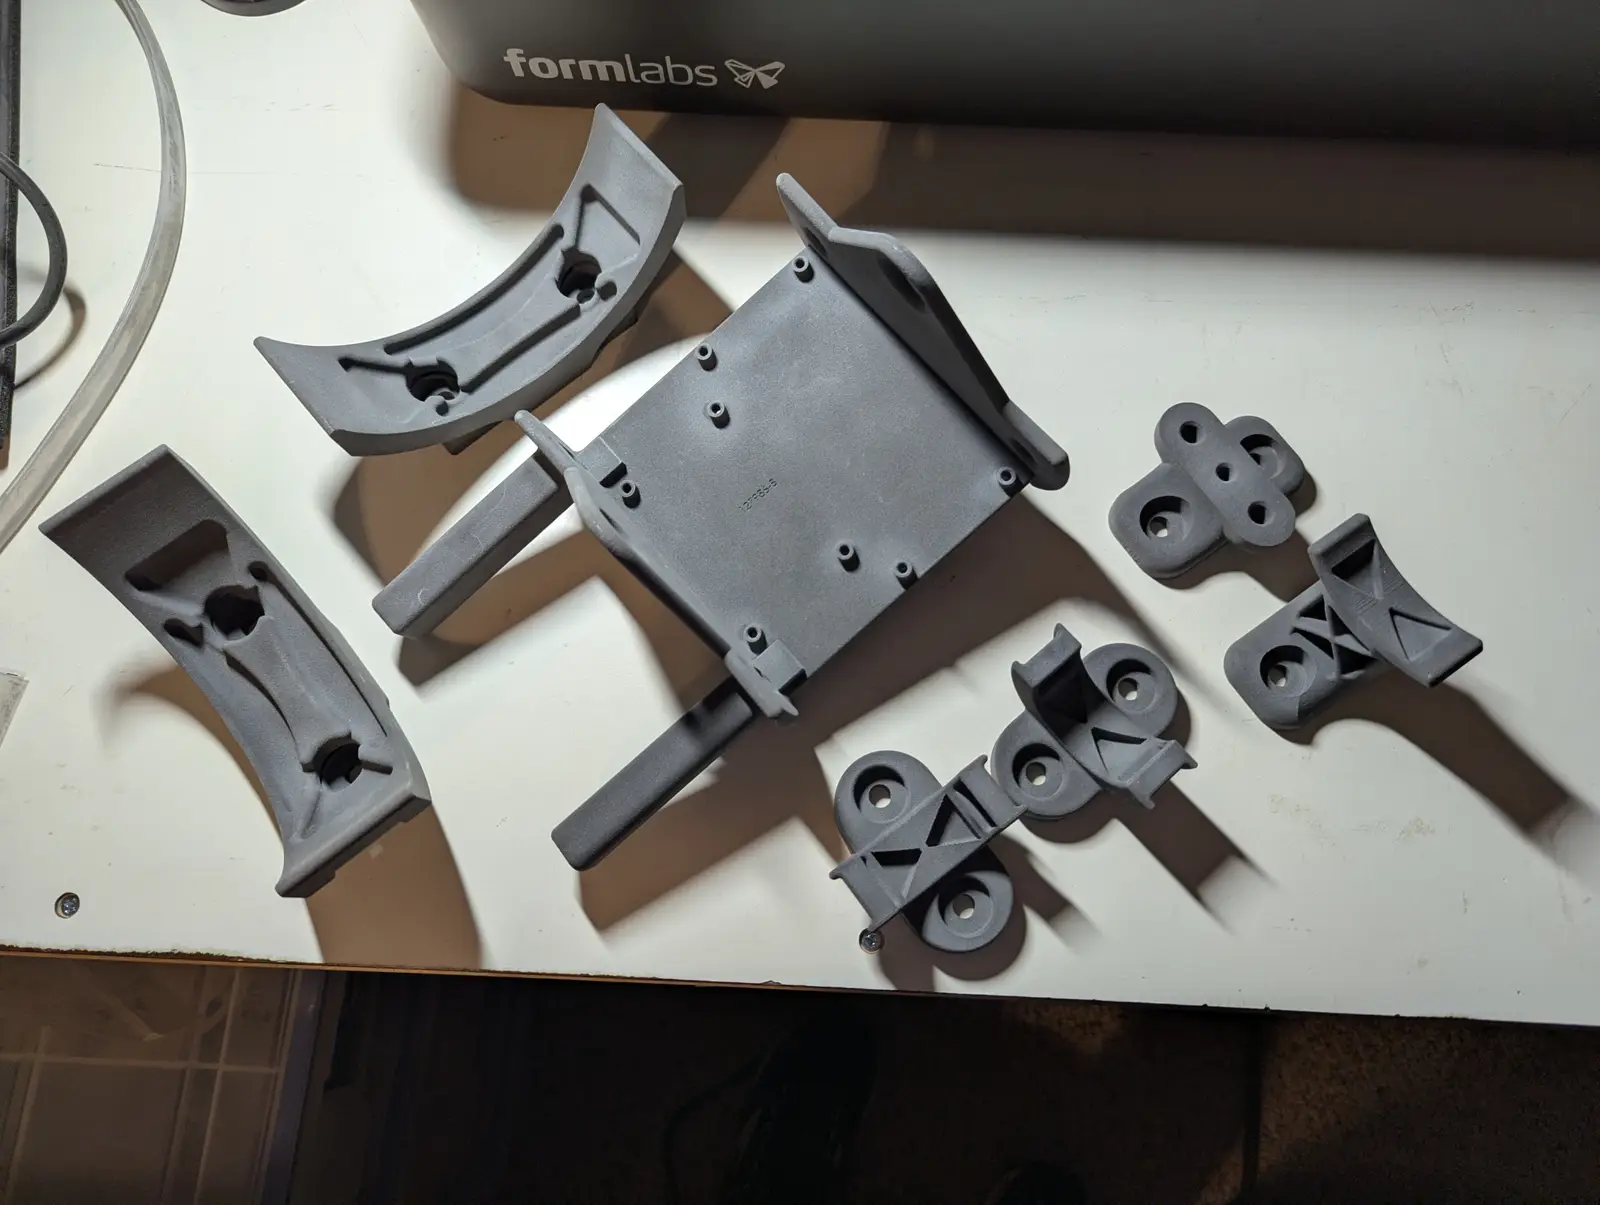 SLSTypical Lead time3-7 daysVolume1-500Durable nylon parts with no tooling and no supports, good for complex geometry and nested batches.
 Sheet MetalTypical Lead time1-2 weeksVolume1-1,000Brackets, panels, and enclosures cut and formed with no hard tooling required at this volume.
A CAD file or a sketch. Free quote in about 24 hours.
The best-fit shop from our network makes it, on your timeline.
Inspected, shipped and tracked in your inbox.
At this run size, cost and lead time depend mostly on whether the part needs tooling at all.
| Approach | Best for | Lead time | Cost |
|---|---|---|---|
| Urethane casting | Molded-feel parts at low volume | Lead time: 1-3 weeks | Cost: $$ |
| Bridge tooling | Ramping to real injection molding | Lead time: 3-5 weeks | Cost: $$$ |
| CNC | Precision parts in any material | Lead time: 1-2 weeks | Cost: $$$ |
| SLS | No tooling, complex geometry | Lead time: 3-7 days | Cost: $$ |
A mold or hard tool has a fixed cost that gets divided across every part it makes. Below a certain volume, a no-tooling process like CNC or SLS almost always costs less per part, even though its per-part price looks higher.
An aluminum bridge tool lets you sell real, injection-molded parts for months while a hardened production mold is machined, instead of waiting for the final tool before you can ship anything.
A single assembly might combine a cast urethane housing, a CNC machined bracket, and an SLS printed bracket. Sourcing each part by what it actually needs beats forcing one process on the whole BOM.
You do not have to commit to one large run. Order in smaller batches as demand firms up, or set a release schedule, so you are not tying up cash in inventory that sits on a shelf.
Upload a part and we'll source low-volume pricing across urethane casting, bridge tooling, CNC, and 3D printing from qualified manufacturing partners.
STEP · STL · IGES · DWG · DXF · SLDPRT · and more
No CAD file? Describe your project instead
Low volume generally means roughly tens to a few thousand parts, above a one-off prototype but below the volume where a hardened production tool pays for itself. The exact line depends on the part: a small simple part might make sense to mold at a few hundred pieces, while a large or complex part might stay on CNC or casting well into the thousands.
For 100 parts, a no-tooling process such as CNC machining or SLS 3D printing is usually cheapest overall, since there is no tool to pay off. If the part needs to look and feel like an injection-molded plastic part, urethane casting from a low-cost silicone tool is often the next cheapest option. The right answer still depends on material, geometry, and finish, so it helps to get quotes across a couple of processes.
Bridge production uses a faster, cheaper tool, typically an aluminum injection mold, to run real parts while a hardened steel production tool is being machined. It lets you sell or field-test actual molded parts during the weeks or months a final tool takes to build, instead of waiting on the production tool before shipping anything.
Tooling is worth it once the volume is high enough that the per-part savings from a molded or stamped process outweigh the fixed tool cost. Below that break-even point, no-tooling processes like CNC or 3D printing usually cost less overall. Ask shops to quote your part both ways, at your current volume and at your expected volume a year out, to see where that crossover lands.
Yes. Parts you have made are saved to your OpenSpindle parts library, so a reorder is a couple of clicks rather than a fresh request, and it can be routed back to the same shop for consistency. For molded or cast parts, the tool stays with the shop that made it, so repeat runs skip the tooling cost and pick up where the last run left off.