 Made on OpenSpindle
Urethane Casting partPrototype Molding
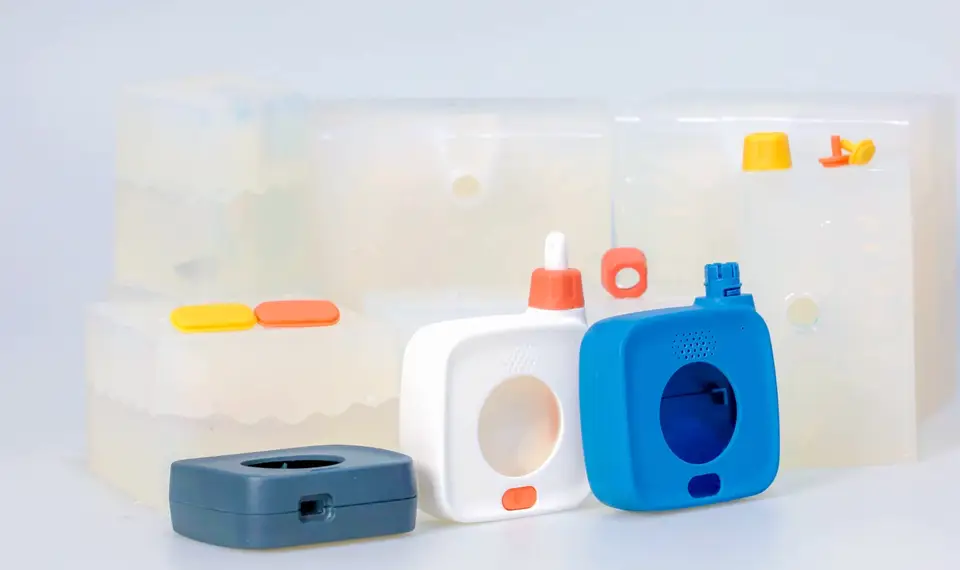
The bridge between a 3D-printed prototype and a full injection-molded production run. A silicone tool is cast off a machined or 3D-printed master, then used to vacuum-cast urethane resins that look and feel like production plastic, roughly 10 to 200 parts per tool at a fraction of hard-tooling cost. Upload your part and we'll send you one matched quote from a qualified manufacturing partner.
STEP · STL · IGES · DWG · DXF · SLDPRT · and more
No CAD file? Describe your project instead
Made on OpenSpindleUrethane casting (vacuum casting) is a process that pours or injects two-part polyurethane resin under vacuum into a silicone mold cast from a 3D-printed or machined master. It produces parts that look and feel like production plastic or rubber, suited to runs of roughly 10 to 200 parts, with each silicone tool typically lasting about 20 to 25 casts.
Last reviewed
Send a part and get a real price. Nothing to commit to, no cost to ask.
One lead from quote to delivery who has sourced it before.
NDA on request. Files shared only with matched shops.
A CAD file or a sketch. Free quote in about 24 hours.
The best-fit shop from our network makes it, on your timeline.
Inspected, shipped and tracked in your inbox.
Two-part polyurethane systems are formulated to mimic the look, feel, and mechanical behavior of common production plastics and rubbers. Filled and flame-retardant grades are available, and shops can also cast clear and translucent parts. If your target material is not here, ask when you request a quote.
Cast urethane parts come off a flexible silicone tool, so the design rules lean similar to injection molding but with looser tolerances and a shorter tool life.
| Design rule | Typical spec | Why |
|---|---|---|
| Nominal wall thickness | 0.060 to 0.150 in | Uniform walls cast and cure evenly. |
| Minimum wall thickness | 0.040 in | Thinner walls risk incomplete fill or fragility once demolded. |
| Draft angle | 1 to 2 degrees per side | Flexible silicone forgives less draft than steel, but draft still eases clean release. |
| General tolerance | ±0.010 in or ±0.003 in/in, whichever is greater | Resin shrinkage and the flexible tool make it looser than machined or steel-molded tolerances. |
| Silicone tool life | ~20 to 25 parts per mold | The tool degrades and tears at parting lines and undercuts; a new tool is recast off the same master. |
| Maximum part size | Bounded by the vacuum casting chamber | Large parts may need to be cast in sections and bonded, or split across multiple tools. |
Exact numbers depend on the resin system and the shop's casting chamber. Send your part and a shop confirms wall, draft, and tolerance for the cast resin you pick.
Urethane casting trades hard tooling for a soft silicone mold, which is what makes it fast and cheap for a low-volume run. These are the tooling choices shops weigh.
The shop picks the method from your CAD, and the quote tells you which.
Urethane casting shops on OpenSpindle support everything from consumer product bridge runs and trade-show samples to low-volume medical and robotics housings.
Urethane casting fills the gap between a printed prototype and a production mold. When your volume, timeline, or material points elsewhere, here is the better-fit process.
| Process | Best for | Typical volume | Choose it over Urethane Casting when |
|---|---|---|---|
| Injection Molding | High-volume production | 1,000+ | You are past a few hundred parts and want the lowest per-part cost and true production resin. A steel or aluminum tool amortizes once volume climbs into the thousands. |
| 3D Printing | One-offs, fastest turnaround | 1 to 50 | You need parts today and can accept as-printed finish and strength. Urethane casting takes longer to set up a tool but delivers more production-like resins and surface quality. |
| CNC Machining | Metal or tightest tolerances | 1 to 500 | The part needs to be metal, or needs a tolerance tighter than a flexible silicone tool can hold. Casting suits plastic-like geometry where machining would be slow or costly. |
The design and sourcing choices that move your tooling cost, per-part price, and lead time.
One silicone tool lasts roughly 20 to 25 casts before it needs replacing. If you need more parts than that, plan for the shop to cast a second tool off the same master rather than pushing a worn mold past its life and risking part quality.
Cast urethanes are formulated to mimic ABS, PP, PC, clear acrylic, or rubber, each with different stiffness, impact resistance, and heat tolerance. Tell the shop what the part needs to do (drop test, flex, chemical exposure) and let them match a resin, not just a color.
The silicone tool is a direct copy of the master, so any sink, print lines, or surface texture on the master transfers to every part cast from it. Sand, polish, or paint the master to the finish you want before it goes into the silicone.
Urethane casting is most valuable for the gap between a printed prototype and a production mold: trade-show samples, user testing, a bridge run while a steel tool is cut. If your volume settles in the thousands, price out injection molding against your ongoing casting cost.
Urethane casting cost is driven by the master pattern, silicone mold making, resin, and the number of parts each mold can produce. The process starts with a master, often 3D printed and hand finished, then a silicone mold is poured around it, and those steps are a fixed cost for each part design. Each silicone mold yields a limited number of castings before it wears, so larger quantities may need more molds. Per-part cost depends on part size and resin, with rigid, flexible, clear, and color-matched urethanes priced differently. Surface finish on the master sets the finish on every casting, so textured or high-gloss requirements add finishing labor. Inserts, painting, and assembly are added steps. Urethane casting fits the gap between 3D printing and injection molding, when you need tens of production-like parts without buying a metal tool. Upload a model and OpenSpindle returns one quote from a matched partner shop.
Urethane casting lead time depends on making the master, curing the silicone mold, the number of castings, and finishing. The master pattern is usually 3D printed and then sanded or finished, and the silicone mold needs time to cure before the first part is poured. Each casting also has to cure in the mold, so a larger quantity, or a quantity that needs several molds, takes longer. Color matching, painting, clear parts that need polishing, and inserted hardware add finishing time. Compared with injection molding, there is no steel or aluminum tool to machine, which is why urethane casting is often used to get production-like parts while a molding tool is being built. After you upload your model, OpenSpindle usually returns one quote in about 24 hours with a lead time for your quantity and finish. Include any date the parts are needed for testing or a launch.
Upload your part and we'll source silicone tooling and per-part pricing for low-volume cast urethane runs from qualified manufacturing partners.
STEP · STL · IGES · DWG · DXF · SLDPRT · and more
No CAD file? Describe your project instead
Urethane casting, also called vacuum casting, makes production-like plastic parts from a silicone mold instead of a machined steel tool. A master pattern (usually 3D printed or CNC machined) is used to cast a silicone tool, then two-part polyurethane resin is poured or injected under vacuum into that tool and cured. It is the standard way to get tens to a couple hundred parts that look and feel molded without paying for hard tooling.
A single silicone tool typically holds up for roughly 20 to 25 casts before it degrades or tears, especially around undercuts and parting lines. Because the master pattern is reusable, a shop can cast additional silicone tools from it if you need more parts than one mold can produce.
Use urethane casting for roughly 10 to 200 parts, when you want a production-like look and feel without paying for a steel or aluminum mold. Move to injection molding once volume climbs into the thousands, since the per-part cost drops sharply once a hard tool is amortized and you gain access to true production thermoplastics. Many programs run a casting bridge while a production mold is being cut.
Cost has two parts: the master pattern and silicone tool, then a per-part cast price. Because the tool is cheap relative to steel and reusable for around 20 to 25 parts, urethane casting is usually far less expensive up front than injection molding for a short run, though the per-part price is typically higher than production molding at volume. Upload your part to see tooling and per-part pricing from qualified manufacturing partners.
Cast resins can be dyed to a target color, and shops offer painting, texture matching, pad printing, and clear or translucent casts for lenses and light pipes. Because the mold is copied off a finished master, the master's surface finish (polished, textured, or matte) transfers directly to every cast part.
A master pattern, first silicone tool, and initial cast parts typically come together in about 1 to 3 weeks, faster than cutting a production mold. Additional parts off the same tool ship quickly after that, and casting several tools in parallel from one master can compress a larger order further.
Yes. Two-part polyurethane systems come in a range of durometers, typically described on the Shore A or Shore D scale, so a shop can cast anything from a soft rubber-like seal or grip to a rigid, plastic-like structural part from resins tuned to match.
Comparing manufacturing services? See Xometry alternatives