 Made on OpenSpindle
Aluminum part, Sheet Metal & Press BrakeAluminum · Sheet Metal & Press Brake
Rack frames, custom-depth enclosures, mounting brackets, adapter rails, blanking panels, and liquid-cooling hardware. Upload your CAD files or drawings and we'll send you one matched quote from a qualified manufacturing partner set up for sheet metal, machining, and welding at buildout scale.
STEP · STL · IGES · DWG · DXF · SLDPRT · and more
No CAD file? Describe your project instead
Made on OpenSpindleSend a part and get a real price. Nothing to commit to, no cost to ask.
One lead from quote to delivery who has sourced it before.
NDA on request. Files shared only with matched shops.
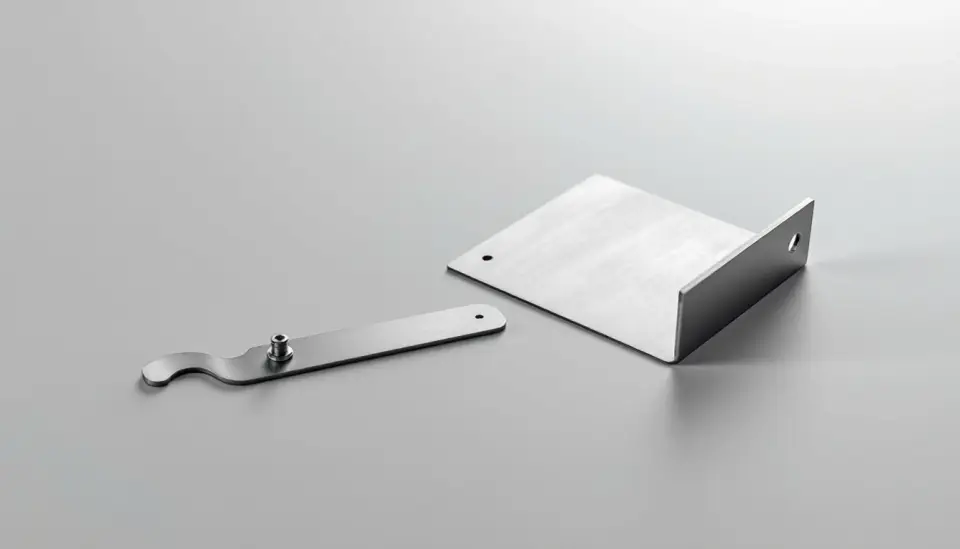
 Sheet Metal FabricationBrackets, rails, panels, shelves, chassis, and rack frames formed from sheet stock.
 Fiber Laser CuttingBlanking panels, brackets, and tray blanks cut fast and to size.
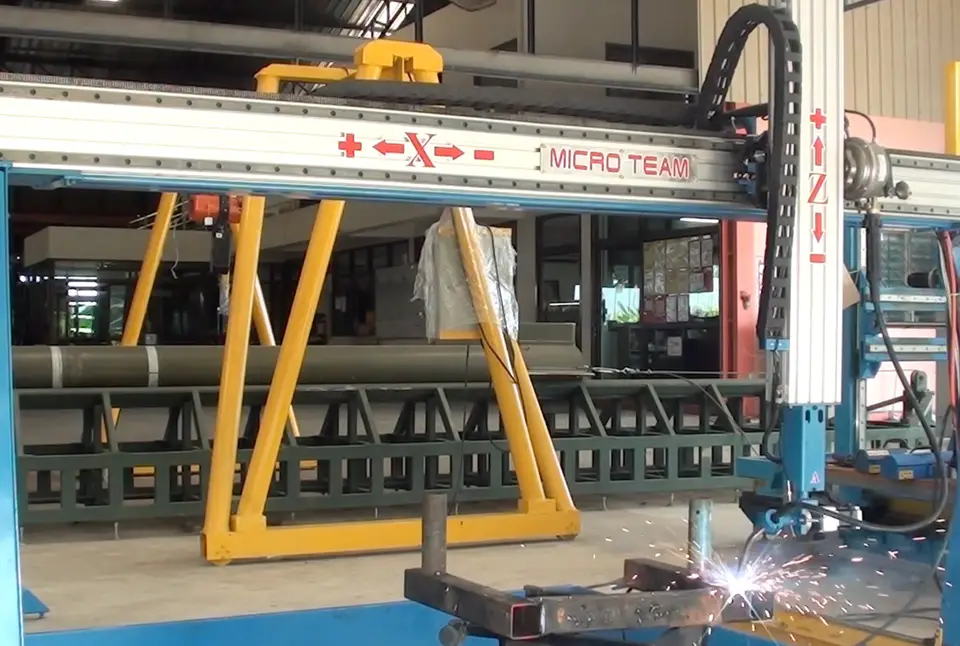 WeldingWelded rack frames, uprights, shelves, and cable tray assemblies.
 Powder CoatingDurable black finish on frames, brackets, panels, and tray, with masking where parts must stay conductive.
 CNC MachiningCold plates, manifolds, and thermal blocks milled from copper and aluminum.
 Waterjet CuttingThick copper and aluminum busbars cut cold with no heat-affected edge.
 CNC TurningCoolant fittings, standoffs, and connector bodies turned to tight tolerances.
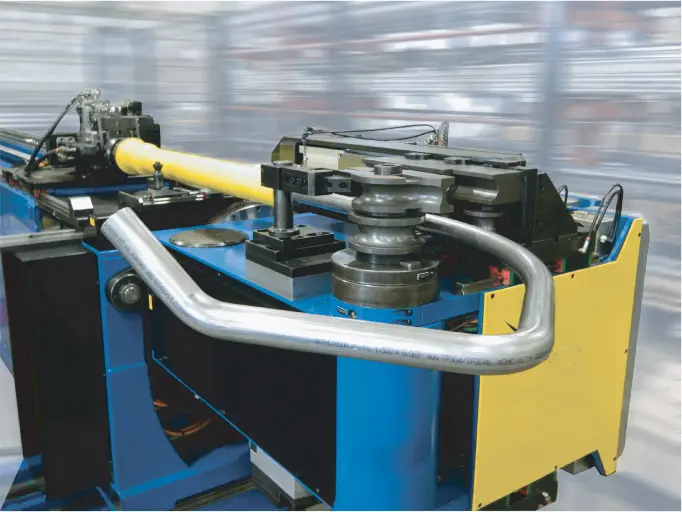 Tube BendingCoolant lines and manifold runs bent for rack-level plumbing.
A CAD file or a sketch. Free quote in about 24 hours.
The best-fit shop from our network makes it, on your timeline.
Inspected, shipped and tracked in your inbox.
Open Rack V2 used a 12 VDC busbar; V3 moved to 48 VDC. Confirm the standard and the frame before cutting rails or brackets.
| Standard | Mounting width | Unit height | Typical enclosure | Where used |
|---|---|---|---|---|
| EIA-310-E, 19 in | 19.0 in (482.6 mm) | 1U = 1.75 in (44.45 mm) | 42U, 45U, 48U, or 52U at 600 or 800 mm wide and 1000 to 1200 mm deep | The default for servers, switches, and most colocation cabinets. Mounting holes repeat in a 0.500, 0.625, 0.625 in pattern up each rail. |
| 23 in telecom | 23 in (584 mm) | 1U = 1.75 in (44.45 mm) | Open two-post and four-post frames | Carrier and telecom equipment. Hole patterns vary by frame and vendor, so confirm the pattern against the frame before cutting rails. |
| OCP Open Rack V3 | 537 mm (nominally 21 in) | 1 OpenU (OU) = 48 mm | External size is set by the rack vendor, not the base spec. Shipped racks are commonly 600 mm wide and about 1070 mm deep | Hyperscale and AI compute. Power comes from a rear 48 VDC busbar with blind-mate connections, so sleds carry no individual power supply. |
The recurring custom work on a buildout or retrofit. Confirm rail standard, thread, and finish with the shop.
| Component | Typical process | Typical material | Notes |
|---|---|---|---|
| Custom brackets and mounting plates | Laser cutting, forming | 16 ga steel, 0.080 in 5052 aluminum | One of the most common one-off rack jobs. Send a flat pattern or a STEP model with hole pattern and thread callouts. |
| Adapter and shelf rails | Laser cutting, forming, welding | 14 ga steel | Adapts equipment of one depth or width to a frame built for another. Call out the rail hole pattern and thread. |
| Blanking panels | Laser cutting, forming | 18 to 20 ga steel, aluminum, polycarbonate | Airflow management. Size to the U height and the rail hole pattern. |
| Cable tray and ladder rack | Laser cutting, forming, welding | 14 ga steel | Powder coated after welding. Note load and span on the drawing. |
| PDU and power mounts | Laser cutting, forming | 16 to 14 ga steel | Tool-less or bolted. Confirm the PDU mounting pattern and whether the bracket sits in the grounding path. |
| Equipment shelves | Laser cutting, forming, welding | 16 to 12 ga steel | Vented or solid. Rate the shelf for equipment weight and note whether it is cantilevered or four-post. |
| Containment panels and end caps | Laser cutting, forming | Sheet aluminum, steel, polycarbonate | Hot or cold aisle containment. Usually built to site measurements, so field dimensions matter more than a model. |
| Air dams and baffles | Laser cutting, forming | 20 ga steel, aluminum, plastic sheet | Blocks bypass air around equipment. Often a flat part with a single bend. |
| Custom-depth frames and uprights | Laser cutting, forming, welding | 12 to 11 ga steel | For equipment that does not fit a stock cabinet. Punch or thread the rails to the standard you are matching. |
| Cage and lock hardware | Machining, laser cutting | Steel, aluminum | Security panels, locking bars, and cage mounts for colocation. |
Steel gauge follows the Manufacturers Standard Gauge for sheet steel. Aluminum is ordered by decimal thickness rather than a gauge number, so specify aluminum in inches or millimeters on the drawing. For the full chart and minimum bend radius by thickness, see the sheet metal gauge and bend radius chart.
| Gauge or thickness | Inches | mm | Typical rack use |
|---|---|---|---|
| Steel, 20 ga | 0.0359 | 0.91 | Air dams, baffles, light covers |
| Steel, 18 ga | 0.0478 | 1.21 | Blanking panels, non-structural covers |
| Steel, 16 ga | 0.0598 | 1.52 | Brackets, chassis panels, light shelves |
| Steel, 14 ga | 0.0747 | 1.90 | Mounting rails, cable tray, heavier brackets |
| Steel, 12 ga | 0.1046 | 2.66 | Shelves and structural brackets |
| Steel, 11 ga | 0.1196 | 3.04 | Rack frames and uprights, seismic bracing |
| Aluminum, 0.063 in | 0.063 | 1.60 | Blanking panels and light covers |
| Aluminum, 0.080 in | 0.080 | 2.03 | Brackets and panels where weight matters |
| Aluminum, 0.125 in | 0.125 | 3.18 | Structural brackets, containment framing |
10-32 and 12-24 screws look similar and are not interchangeable. Confirm the thread before ordering hardware.
| Rail type | Hole | Fastener | Notes |
|---|---|---|---|
| Square hole (cage nut) | 9.5 mm square | Cage nut with an M6 or 10-32 screw | The most common rail on modern cabinets. Cage nuts let one frame accept several thread sizes. |
| Threaded round hole | Tapped | 10-32 UNF | A common pre-threaded standard on North American 19 in racks, alongside 12-24 and M6. Most modern cabinets use square-hole rails instead. |
| Threaded round hole | Tapped | 12-24 UNC | Found on older frames and some telecom racks. |
| Threaded round hole | Tapped | M6 | Common on frames specified in metric. |
| Clearance round hole | Unthreaded, 6.6 mm normal fit or 7.0 mm loose for M6 | Screw with a nut, or a cage nut | Used where the fastener passes through and captures a nut behind the rail. |
For busbars, call out material and temper, thickness and width, hole pattern, minimum bend radius, edge break, plating (tin, nickel, or silver), and joint torque. Continuous current rating depends on temperature rise, orientation, ventilation, plating, and altitude, so size the bar against the standard that applies to your installation rather than a single published figure.
| Component | Typical process | Typical material | Notes |
|---|---|---|---|
| Cold plates | CNC machining | Copper C110, aluminum 6061 | Machined channels or a skived fin field. Flatness and finish on the die-facing surface drive thermal performance. |
| Cooling manifolds | CNC machining, tube bending | Aluminum, stainless steel | Distribute coolant to the cold plates. Leak-tested before shipping. |
| Busbars and power distribution | Waterjet, machining | Copper C110, aluminum 1350 | Plated contacts keep high-current joints low-resistance. |
| Coolant fittings and connector bodies | CNC turning | Brass, stainless steel | Put thread form, seal type, and pressure rating on the drawing. |
We do not publish price ranges for this work: the spread across material, joining method, and test requirements is wider than a range would honestly represent. Upload a drawing for a real quote sourced from our shop network.
| Driver | Pushes cost down | Pushes cost up |
|---|---|---|
| Material | 5052 aluminum, cold-rolled steel | Copper C110, stainless steel |
| Process | Laser cut and formed from flat stock | Machined from solid, or welded and ground assemblies |
| Joining | Bolted or gasketed two-piece designs | Vacuum brazing, friction stir welding, seam welding |
| Tolerance | Standard sheet metal tolerances | Flatness callouts on thermal contact faces, tight hole-to-hole position |
| Finish | Mill finish or as-cut | Powder coat with masking, selective plating, cosmetic requirements |
| Testing and certification | None | Pressure or leak test with a certificate, material certs, first article inspection |
| Quantity | Repeat orders that amortize setup and nest efficiently | One-off parts carrying full setup |
| Geometry | Consistent bend directions and standard hardware | Many setups, tight bend reliefs, custom hardware |
Finding a shop that will prototype a cold plate or a custom rack takes days of cold outreach. Upload your design once and surface independent shops already set up for thermal and rack hardware, so you spend your time on the system.
Cold plates and busbars fail on flatness, cleanliness, and resistance. We match your part to shops that hold flatness on contact faces, leak-test sealed assemblies, and coordinate the plating your busbars need.
Most data center fabrication is not a new product, it is fitting equipment into a frame that was not built for it. Send brackets, rails, and custom-depth frames for one all-in quote, and we can keep the same shop as the same part repeats across rows and sites.
Upload a drawing and get a real quote sourced from qualified manufacturing partners, without a sales call first. Faster than login-walled portals.
Data center fabrication is driven more by fit, finish, and electrical and thermal performance than by formal vertical certifications. These are the signals worth confirming with a shop before you place an order.
The general quality management baseline you will see on most precision shops. It signals documented, repeatable processes for scaling a validated bracket, rail, or cold plate into a deployment.
Ask whether the shop has built to EIA-310-E, to a 23 in telecom frame, or to OCP Open Rack, and confirm they will punch or thread rails to the standard your frame uses. A rail cut to the wrong hole pattern is scrap.
Confirm the shop can mask contact areas, apply chromate conversion coating where a joint must stay conductive, and hold gasket channels and fastener spacing on parts that close a shielded enclosure.
Powder coat color and texture, zinc or selective plating, anodize type, and which surfaces are masked. Get these on the drawing so finishing is quoted rather than discovered.
The core requirement for liquid cooling. Ask whether the shop can pressure- or leak-test sealed cold plates and manifolds, how it joins them, and whether parts are deburred, washed, and capped so they arrive ready to plumb.
A cold plate only works if it makes contact. Confirm the shop can hold flatness on the die-facing surface and produce the specified finish for thermal-interface contact.
Upload your drawing and we'll send you one matched quote from a qualified manufacturing partner set up for rack frames, brackets, rails, panels, and cooling hardware.
STEP · STL · IGES · DWG · DXF · SLDPRT · and more
No CAD file? Describe your project instead
The dominant standard is EIA-310-E, a 19 inch rack: 19.0 in (482.6 mm) of equipment mounting width, with height counted in rack units where 1U equals 1.75 in (44.45 mm). Mounting holes repeat in a 0.500, 0.625, 0.625 in pattern up each rail. Full cabinets are commonly 42U, 45U, 48U, or 52U tall, 600 or 800 mm wide, and 1000 to 1200 mm deep. Telecom frames use a 23 in mounting width, and OCP Open Rack V3 uses a 537 mm equipment width, nominally 21 in, with a 48 mm OpenU.
Yes. Custom-depth frames are routine sheet metal and welding work, and they are one of the more common reasons buyers come to a fabrication shop instead of buying a stock cabinet. Give the shop the equipment depth, the rail standard and thread you are matching, the U height you need, and the floor and overhead constraints at the site. Frames and uprights are typically 12 to 11 gauge steel, powder coated after welding.
Yes, and it is one of the most common one-off data center jobs. Brackets and adapter rails let equipment of one depth, width, or mounting pattern fit a frame built for another. Send a flat pattern or a STEP model with the hole pattern, thread callout, material, and finish. Brackets are usually 16 gauge steel or 0.080 in 5052 aluminum, and adapter rails that carry weight are usually 14 gauge.
It depends on the part. Blanking panels and light covers are typically 18 to 20 gauge, brackets and chassis panels 16 gauge, mounting rails and cable tray 14 gauge, and frames, uprights, and heavy shelves 12 to 11 gauge. Aluminum is a separate case: it is ordered by decimal thickness rather than by a steel gauge number, so specify aluminum parts in inches or millimeters on the drawing.
A 19 inch EIA-310-E rack gives 19.0 in of mounting width and counts height in 1.75 in rack units, and each piece of equipment brings its own power supply. OCP Open Rack V3 widens the equipment opening to 537 mm, nominally 21 in, changes the height increment to a 48 mm OpenU, and moves power to a shared 48 VDC busbar at the rear that sleds blind-mate into. The two are not interchangeable, so brackets, rails, and blanking panels have to be made for the standard the frame uses.
Yes. These are straightforward laser-cut and formed sheet metal parts and shops make them in quantity. Blanking panels need the U height and the rail hole pattern. Cable tray and ladder rack need load and span. Containment panels and end caps are usually built to site measurements rather than to a model, so accurate field dimensions matter more than a CAD file.
Often, yes. The fabrication side of that retrofit is usually brackets, custom-depth rails, reinforced or re-rated shelves, PDU and busbar mounts, and revised blanking or containment for airflow. Whether the retrofit is viable at all depends on floor loading, power, and cooling capacity at the site, which is an engineering question ahead of the fabrication. Bring the frame make and model, the rail standard, and the equipment you are trying to fit.
Black powder coat is the default for steel rack parts and gives a durable, low-glare surface. Zinc plating is common on hardware. Aluminum can be anodized or powder coated. One caution: anodizing is electrically insulating, so if a bracket or panel sits in a grounding or bonding path, use chromate conversion coating instead, or mask the contact area, so the joint stays conductive.
They mostly change the finish and the joint rather than the geometry. Any part in a bonding path needs a conductive contact area, which means masked powder coat, chromate conversion coating, or a paint-piercing washer and star washer at the joint. Parts that close an enclosure for shielding need attention to seams, gasket channels, and fastener spacing. Put bonding points, masked areas, and any gasket requirement on the drawing so the shop quotes the masking rather than discovering it later.
Yes. Independent shops machine cold plates from copper and aluminum, milling internal channels or a skived or machined fin field, then sealing the plate by brazing, friction stir welding, or a gasketed two-piece design. Call out the coolant, working pressure, flatness on the die-facing surface, and any leak-test requirement so the shop quotes the right process.
Yes. Sheet metal shops fabricate server chassis and sleds: cutting, punching, forming, and finishing to rack-unit dimensions, with cutouts and standoffs for drives, boards, and airflow. Send a flat pattern or STEP model with material, finish, and any EMI, airflow, or mounting requirements, and note the quantity so the shop can quote the right process.
Yes. Shops cut and machine busbars from copper (typically C110) and aluminum, including waterjet-cut blanks, bent geometry, and drilled or tapped connections. Because contact resistance drives heat, note flatness on mating faces and any tin, nickel, or silver plating on the drawing.
Many will. Ask up front whether the shop can pressure- or leak-test sealed cold plates and manifolds to your spec and provide a certificate. If the loop must arrive clean, specify deburring, washing, and capping so the parts are ready to plumb into a system.
Yes. A single prototype cold plate, manifold, or rack is normal work for independent shops and the right way to validate before committing to volume. Note the quantity and target date, and expect a setup charge on one-offs that drops on repeat orders.
A STEP or IGES model plus a dimensioned PDF drawing calling out material and alloy, flatness and surface finish on thermal contact faces, plating on busbars, coolant and pressure for cooling parts, tolerances, and quantity. For sheet parts, a flat pattern or DXF helps. Flag any leak-test or cleanliness requirements so shops quote them in.
Last reviewed