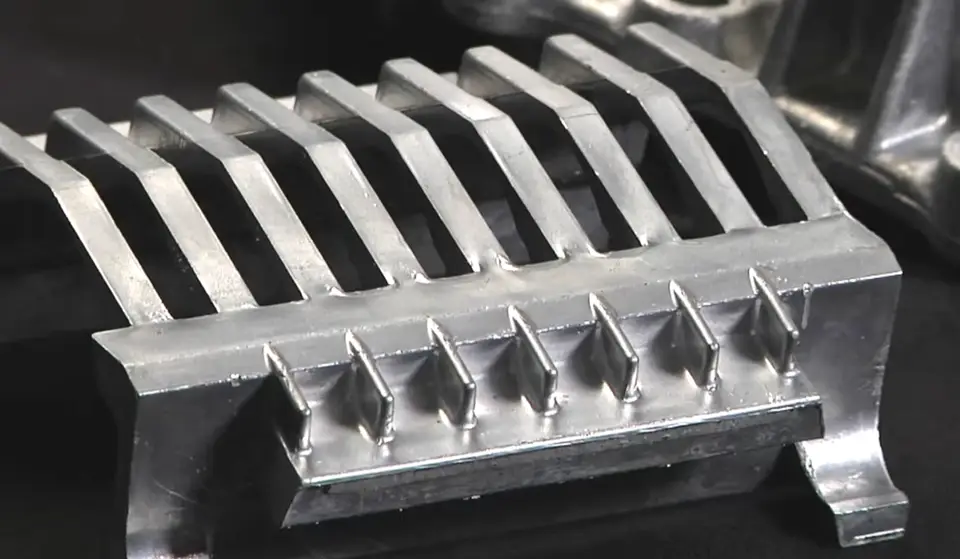
 Made on OpenSpindle
Die Casting partMade on OpenSpindle
Molten metal is forced under high pressure into a hardened steel die, producing strong, dimensionally stable metal parts with tight repeatability, shot after shot. Once the tooling is paid off, die casting is the lowest per-part cost way to make a metal part at volume, in aluminum, zinc, or magnesium. Upload your part and we'll send you one matched quote from a qualified manufacturing partner.
STEP · STL · IGES · DWG · DXF · SLDPRT · and more
No CAD file? Describe your project instead
Made on OpenSpindleDie casting is a metal casting process that forces molten aluminum, zinc, or magnesium under high pressure into a hardened steel die. It produces strong, dimensionally stable net-shape or near-net-shape parts like housings and brackets, and once tooling is paid off it offers a low per-part cost at volume. As-cast tolerance is roughly ±0.004 in for the first inch.
Last reviewed
Send a part and get a real price. Nothing to commit to, no cost to ask.
One lead from quote to delivery who has sourced it before.
NDA on request. Files shared only with matched shops.
A CAD file or a sketch. Free quote in about 24 hours.
The best-fit shop from our network makes it, on your timeline.
Inspected, shipped and tracked in your inbox.
The common die casting alloys and where each fits. Zinc (Zamak) leads for thin walls and fine detail, aluminum for lightweight structural parts, magnesium for the best strength-to-weight. Values are typical ranges; a shop confirms against its process.
| Alloy | Tensile | Hardness | Min wall | Best for |
|---|---|---|---|---|
| Zinc · Zamak 3 | 280 MPa | 82 HB | 0.5 mm | The default zinc: castability, fine detail, plating |
| Zinc · Zamak 5 | 330 MPa | 91 HB | 0.5 mm | More strength and hardness than Zamak 3 |
| Zinc · ZA-8 | 370 MPa | 100 HB | 0.6 mm | Higher-strength zinc, hot-chamber castable |
| Aluminum · A380 | 324 MPa | 80 HB | 1.0 mm | Lightweight structural parts, good all-rounder |
| Aluminum · ADC12 | 310 MPa | 80 HB | 1.0 mm | A380 equivalent common in Asian supply |
| Magnesium · AZ91D | 230 MPa | 63 HB | 1.0 mm | Lightest option, best strength-to-weight |
Zinc alloys run on hot-chamber machines and hold the thinnest walls and tightest detail; aluminum runs cold-chamber; magnesium is the lightest structural choice. Tell the shop the part's loads, weight target, and finish and they recommend the alloy.
Die cast parts live or die by wall design and how cleanly metal flows and fills the die. These rules keep parts free of porosity, sink, and short shots.
| Design rule | Typical spec | Why |
|---|---|---|
| Minimum wall thickness | 0.030 to 0.060 in (alloy-dependent) | Zinc can run thinner than aluminum; thinner walls fill faster but need more precise gating. |
| Draft angle | 1 to 3 degrees per side | Lets the part release cleanly from the die; deeper cavities and textured surfaces need more. |
| Standard tolerance | ±0.004 in for the first inch, plus roughly ±0.001 in per additional inch | Tighter features are held with secondary CNC machining after casting. |
| Fillet / corner radius | ≥ 1x wall thickness | Sharp internal corners restrict metal flow and concentrate stress, driving porosity and die wear. |
| Rib thickness | ≤ 0.75x adjacent wall | Thicker ribs cool slower than the wall and pull a visible sink mark on the opposite face. |
| Section thickness for porosity | Keep sections under about 0.25 in where possible | Thick sections cool slower and trap gas, causing internal porosity; core out mass where the part allows it. |
| Maximum part size | Alloy- and machine-dependent, typically limited by press locking force | Larger projected area needs a higher-tonnage press to hold the die shut against injection pressure. |
Exact limits depend on the alloy and the part geometry. Send your drawing and a shop tunes gates, wall thickness, and draft to it.
The die is the biggest driver of your cost, lead time, and per-part price, and the casting method depends on your alloy. These are the choices die casters weigh, from a single-cavity die to a full production tool.
The shop picks the method from your CAD, and the quote tells you which.
Die casting shops on OpenSpindle make parts for everything from automotive brackets and housings to consumer electronics enclosures and lighting fixtures.
Die casting wins on per-part cost and repeatability for metal parts at volume, once its tooling is paid off. When your volume, material, or geometry points elsewhere, here is the better-fit process.
| Process | Best for | Typical volume | Choose it over Die Casting when |
|---|---|---|---|
| Injection Molding | Plastic parts | 1,000 to 1,000,000+ | Your part is plastic, not metal. Injection molding shares the same tooling logic (steel mold, multi-cavity, runner systems) but processes thermoplastics instead of molten metal. |
| Sand Casting | Large or very low-volume metal parts | 1 to 500 | You need a handful of large or one-off metal parts where a hardened die is not worth the tooling spend. Sand casting tooling costs far less, but the process is slower and holds looser tolerances per part. |
| CNC Machining | Low-volume metal / tightest tolerance | 1 to 1,000 | You need a few to a few hundred metal parts with no tooling lead time, or tolerances tighter than as-cast surfaces can hold. Die casting takes over once volume justifies the die. |
| Metal Stamping | Flat or formed sheet metal at volume | High | Your part is flat or sheet-formed rather than a true 3D net shape. Stamping tooling is typically cheaper than a casting die and runs faster for simple sheet geometries. |
Die casting cost combines a one-time die cost with a per-part cost, and it usually makes economic sense at higher volumes. The steel die is a significant investment that grows with part size, complexity, the number of cavities, and slides for undercuts. Per-part cost depends on alloy, part weight, and cycle time, with aluminum and zinc alloys being the most common. Most die cast parts need trimming, and many need machining of bores, threads, or sealing faces, plus finishing such as powder coat or plating, and those steps can be a large share of the part price. Design choices such as uniform walls, draft, and generous radii improve fill and reduce scrap. Porosity requirements and leak testing add cost. For lower quantities, sand casting, investment casting, or CNC machining may cost less in total. Share your annual volume when you upload a model, and OpenSpindle returns one quote from a matched casting partner.
Die casting lead time for a new part is led by designing and building the die, followed by sampling and approval, then production. Steel dies take substantial time to design and machine, and first shots are inspected and adjusted before production is approved. Once the die is proven, production depends on the matched partner's machine schedule, the run quantity, and the secondary operations each part needs. Trimming, machining of critical features, impregnation for pressure-tight parts, and finishing such as powder coat or plating each add a step. Repeat orders on an existing die skip tooling and move much faster. After you upload your files, OpenSpindle usually returns one quote in about 24 hours with tooling and production lead times. Include your target launch date and annual volume in the request so the job is matched to a partner with the right machine size and capacity.
Upload your part and we'll source tooling and per-part pricing from qualified manufacturing partners for aluminum, zinc, and magnesium.
STEP · STL · IGES · DWG · DXF · SLDPRT · and more
No CAD file? Describe your project instead
Die casting is a metal casting process where molten metal, typically aluminum, zinc, or magnesium, is forced under high pressure into a hardened steel die (mold). The metal solidifies quickly in the shape of the cavity, producing a strong, dimensionally stable net-shape or near-net-shape part. Because the die is reusable, the process is well suited to producing thousands to millions of identical metal parts once tooling is cut.
Aluminum is lighter, stronger per pound, and more corrosion-resistant, making it the default for structural brackets, housings, and automotive parts. Zinc is denser but has a lower melting point, casts thinner walls and finer detail, holds tighter tolerances, and typically costs less per part and wears the die more slowly. If your part is small, thin-walled, and cosmetic, ask about zinc; for structural or weight-sensitive parts, aluminum is the usual choice.
Die casting tooling generally runs higher than injection molding tooling for a comparable part, because the die has to withstand molten metal instead of plastic. A simple single-cavity die often starts around $5,000 to $15,000, with multi-cavity or complex production dies running $20,000 to $100,000 or more. Cavity count, part complexity, undercuts, and expected shot life all drive the number. Upload your part to see real tooling and piece pricing from qualified die casting partners.
Hot-chamber machines keep the injection mechanism submerged in a built-in furnace of molten metal, giving faster cycle times. They are used for zinc, magnesium, and other low-melting-point alloys that will not corrode the machine. Cold-chamber machines ladle molten metal into a separate shot sleeve for each cycle and are required for aluminum, since aluminum would corrode a hot-chamber system. Cold-chamber cycles run slower, but it is the standard method for aluminum die casting.
A common as-cast tolerance is roughly +/-0.004 in for the first inch of a dimension, with an additional allowance per inch beyond that, though the exact figure depends on the alloy, part size, and die design. Features that need tighter tolerances than that are typically held with a secondary CNC machining operation after casting rather than by the die alone. Flag the few features that are truly critical on your drawing and the shop can machine those to spec.
Die casting produces metal parts (aluminum, zinc, magnesium); injection molding produces plastic parts. The two processes share a lot of tooling logic, hardened steel tooling, multi-cavity dies, similar draft and wall-thickness rules, but die casting handles far higher pressures and temperatures because it is casting molten metal rather than injecting molten plastic. Choose based on what your part needs to be made of, not on volume alone, since both processes scale to high volumes once tooling is cut.
Comparing manufacturing services? See Xometry alternatives