 Made on OpenSpindle
Metal Stamping partMade on OpenSpindle
Presses and dies turn coil or sheet into formed metal parts at volume, the lowest per-part cost for flat and lightly formed metal once the die is built. Upload your part and we'll send you one matched quote from a qualified manufacturing partner.
STEP · STL · IGES · DWG · DXF · SLDPRT · and more
No CAD file? Describe your project instead
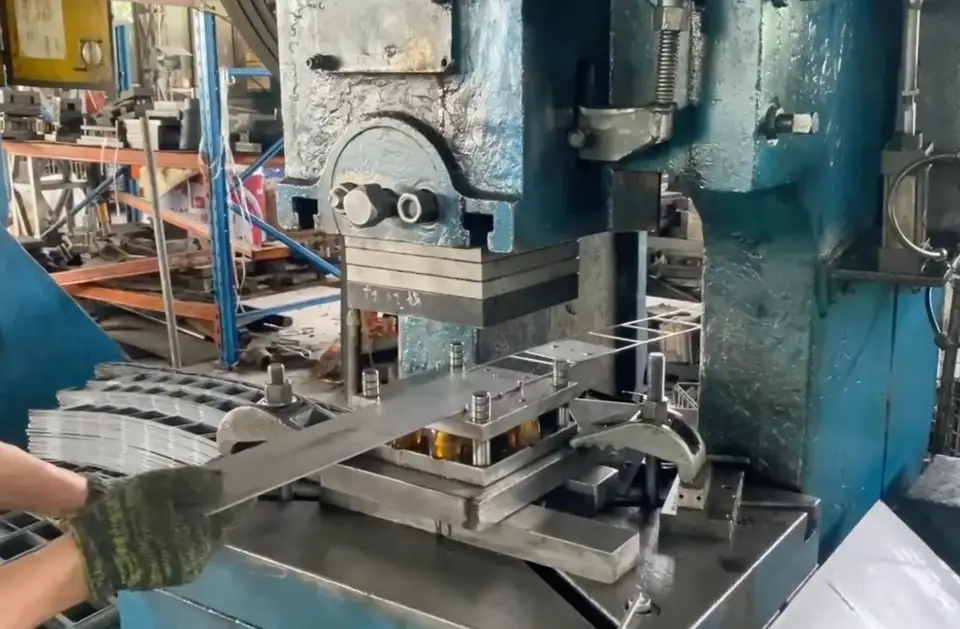
Made on OpenSpindleMetal stamping is a process that uses a press and a die to cut, pierce, bend, and form sheet or coil metal into parts. It suits brackets, terminals, and formed components at high volume, where die cost spreads across thousands or millions of parts. Progressive dies commonly hold about ±0.005 in once the tool is proven out.
Last reviewed
Send a part and get a real price. Nothing to commit to, no cost to ask.
One lead from quote to delivery who has sourced it before.
NDA on request. Files shared only with matched shops.
A CAD file or a sketch. Free quote in about 24 hours.
The best-fit shop from our network makes it, on your timeline.
Inspected, shipped and tracked in your inbox.
Stamping starts from coil or sheet stock. Common metals are below; if your material or temper is not here, ask when you request a quote.
The design choices that most affect whether a stamped part runs cleanly in the die and quotes well.
| Design rule | Typical spec | Why |
|---|---|---|
| Min hole diameter | ≥ material thickness | Smaller holes risk punch breakage during the stroke. |
| Min edge distance | ≥ 2x thickness | Holes or features too close to a part edge distort or tear when the slug is cut free. |
| Min bend radius | ≥ 1x thickness | Tighter radii crack the outside of a formed flange, especially in harder tempers. |
| Typical tolerance | ±0.005 in | Progressive dies hold this on formed features once the tool is proven out; tighter callouts add die cost. |
| Min feature-to-feature spacing | ≥ 2x thickness | Adjacent holes or slots too close together weaken the web between them and can tear during stamping. |
| Internal corner radius | ≥ 0.5x thickness | Sharp internal corners concentrate stress and are a common tear point in blanked or formed profiles. |
Typical starting points for cold-rolled steel and aluminum. Stainless and spring steel are less forgiving; a shop confirms against your part and temper.
The die is the biggest driver of your upfront cost, lead time, and per-part price at volume. These are the tooling choices stamping shops weigh.
The shop picks the method from your CAD, and the quote tells you which.
Stamping shops on OpenSpindle build brackets, terminals, enclosures, and formed components for a wide range of high-volume industries.
| Instead of | Send this |
|---|---|
| "Stamped bracket, need a quote" | "0.062 in cold-rolled steel, blank and form, qty 50,000/yr, progressive die" |
| "Some holes and a bend" | "Hole and bend locations per the flat DXF, tolerances called out on critical features" |
| "Deep drawn part" | "Deep-drawn cup, 1.5 in draw depth, 304 stainless, qty 100,000/yr" |
Material, thickness, annual volume, and whether a die already exists are what set the tooling cost and the per-part price. Send a flat DXF or 3D model with your request.
Stamping wins on per-part cost at volume once the die is paid off. When your volume or geometry points elsewhere, here is the better-fit process.
| Process | Best for | Typical volume | Choose it over Metal Stamping when |
|---|---|---|---|
| Laser Cutting | Flat parts, no tooling | Prototype to low volume | You need flat or lightly formed parts fast, in small quantities, without paying for a die. |
| CNC Machining | Thick or 3D precision parts at low volume | 1 to 1,000 | The part needs 3D machined features or tolerances tighter than a stamped part holds, at a volume too low to justify a die. |
| Sheet Metal & Press Brake | Low-to-mid volume bending and forming | Prototype to mid volume | You need bent or formed sheet metal without a hard die, or the volume does not clear the break-even point for tooling. |
| Die Casting | 3D solid metal parts at volume | 10,000+ | The part is a complex 3D solid shape rather than a formed sheet, and die casting is the better fit for that geometry at volume. |
The design and sourcing choices that move your tooling cost, piece price, and lead time.
A die is a fixed upfront cost that only pays off at volume. If you are not yet confident in your annual quantity, laser cutting or sheet metal fabrication keeps you flexible until the design and demand are locked.
Holes and slots too close to an edge, a bend, or another feature distort or tear as the slug is cut free. Keep spacing at roughly 2x material thickness as a starting point.
Mixing gauges or metals means a different die or a secondary operation. A single material and thickness keeps the part on one progressive die.
If you are reordering a part with an existing die at a shop, say so. You only pay the per-part run cost, not tooling again, unless the die needs a transfer or rework.
Metal stamping cost has two parts, a one-time die cost and a per-part cost, and the right balance depends on your volume. The die is often the largest single expense, and it grows with part complexity, the number of stations in a progressive die, and the die steel needed for long runs. Once the die exists, each part costs mainly material plus press time, which is why stamping becomes very economical at high quantities. Material is usually the biggest per-part cost, so blank size and how well parts nest on the coil strip matter. Tight tolerances, deep draws, and secondary steps such as tapping, plating, or assembly add cost. For low quantities, laser cutting and press brake forming often cost less in total because there is no die to buy. Share your annual volume when you upload a model, and OpenSpindle returns one quote from a matched stamping shop.
Metal stamping lead time is usually dominated by die design and build for a new part, then by press scheduling and material for production runs. A new progressive or compound die takes time to design, machine, and try out, and first parts are checked against the drawing before production is approved. Simpler dies are faster to build than complex progressive tooling. Once a die is proven, a production run depends mainly on the matched shop's press schedule and coil or sheet availability, and presses can produce large quantities quickly. Plating, heat treatment, and assembly add steps after stamping. If you already own a die, the shop may need to inspect it and fit it to its press before running. After you upload your files, OpenSpindle usually returns one quote in about 24 hours with tooling and production lead times. Include your target launch date and annual volume in the request.
Upload your part and we'll source tooling and per-part stamping pricing from qualified manufacturing partners.
STEP · STL · IGES · DWG · DXF · SLDPRT · and more
No CAD file? Describe your project instead
Metal stamping is a manufacturing process that uses a press and a die to cut, pierce, bend, and form flat sheet or coil metal into a part in one or more strokes. It is built for high volume, where the cost of the die is spread across thousands or millions of parts to reach a very low per-part price.
A progressive die is a single tool with a sequence of stations that a strip of coil steps through, one press stroke at a time. Each station performs an operation, blanking, piercing, or forming, and the finished part is cut free from the strip at the last station. It is the standard tool for high-volume stamped parts.
A simple single-station die can run a few thousand dollars, while a multi-station progressive die for a complex part can run tens of thousands. Cost scales with the number of stations, part complexity, tolerances, and expected tool life. Upload your part to get a real tooling quote from qualified stamping partners.
Laser cutting has no tooling cost and is the right call for prototypes and low-to-mid volumes. Stamping needs a die, which is an upfront investment, but once the die is built the per-part cost drops well below laser cutting at high volume. The crossover point depends on part complexity and annual quantity, so ask shops to quote both.
Progressive dies commonly hold about +/-0.005 in on formed and pierced features once the tool is proven out, with tighter tolerances possible on specific critical features at added die cost. Flag the few dimensions that truly matter and a shop tools the die to hold them.
Deep drawing is a stamping operation that forms a flat sheet blank into a hollow, cup-shaped part, such as a can, housing, or enclosure, by pulling the metal into a die cavity rather than just bending it. It takes more press force and a die designed to control material flow so the part does not tear or wrinkle as it forms.
Stamping is a volume process because of the die cost, so most shops look for production quantities, typically in the thousands per year and up, to make sense of tooling a new die. For lower volumes, laser cutting or sheet metal fabrication is usually the better fit until your quantity grows.
Comparing manufacturing services? See Xometry alternatives